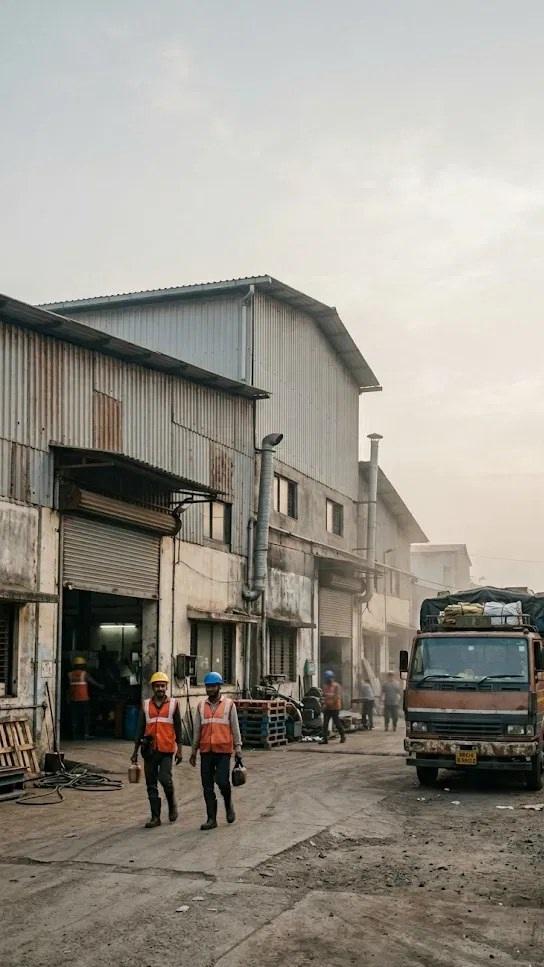
A complete technology partner for Indian manufacturing plants
India's manufacturing sector is under pressure to modernise — tighter safety regulations, leaner operations, complex multi-shift workforces and rising cyber-threats all demand robust technology infrastructure. ITSPL brings 25+ years of industrial deployment experience, delivering integrated solutions that improve uptime, security and operational visibility across the factory floor.
In this guide you will find detailed information on every solution we offer for manufacturing plants — from plant networking and CCTV to fire alarm systems and IT infrastructure. Each solution is described with the specific options and variants we deploy, so you can identify exactly what fits your facility.
We invite you to explore, and we look forward to a conversation about your plant.
The ITSPL Team
Iditri Techno Solutions Pvt Ltd
Unmanned entry points, unmonitored warehouses and manual visitor logs create safety risks and compliance vulnerabilities that auditors increasingly flag.
Production lines and ERP systems depend on stable connectivity; patchy Wi-Fi, ageing switches and no redundancy translate directly into costly downtime.
Multi-shift operations with contract labour make accurate attendance, shift-wise headcount and payroll compliance a persistent operational challenge.
Unmanaged endpoints, no data backup discipline and expired software licences expose the business to ransomware, data loss and regulatory non-compliance.
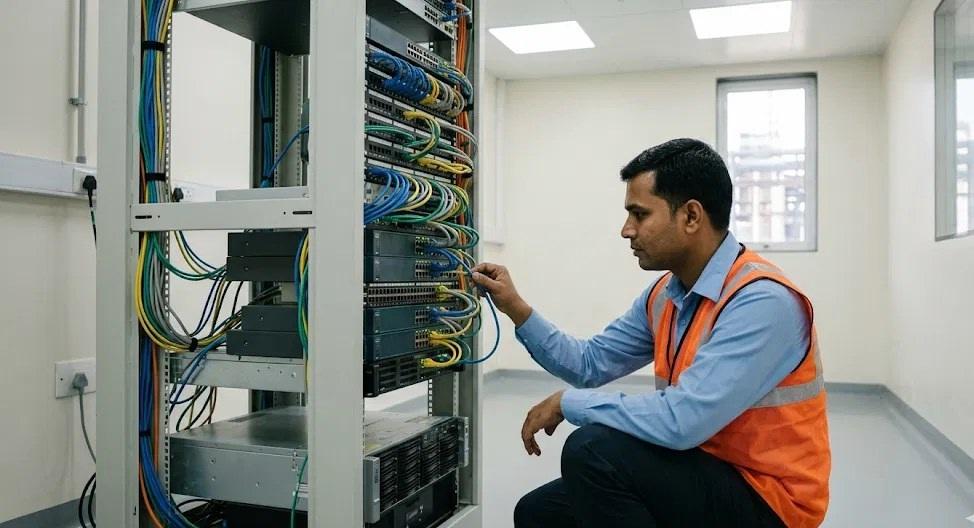
A high-availability structured-cabling and wireless backbone designed for the demands of the factory floor — handling everything from ERP terminals and IP phones to IoT sensors and industrial automation, with ring-topology redundancy and centralised network management.
A certified Cat6A copper and OFC fibre backbone laid across production lines, warehouses and admin blocks. Every run is tested, labelled and documented so future moves, additions and changes are quick and traceable.
DIN-rail managed switches built for extended temperature ranges, dust and vibration on the shop floor. PoE ports power cameras, access points and IP phones directly, removing the need for separate power runs.
High-density access points engineered for roaming across production halls, yards and parking areas without dropped connections. Designed to handle handheld scanners, tablets and supervisor devices on a single seamless network.
A self-healing fibre ring topology that reroutes traffic in milliseconds if any link is cut or a switch fails. Production-critical systems stay online even during cable damage or hardware faults.
A centralised monitoring dashboard giving real-time visibility of every switch, port and access point. Bandwidth reports, fault alerts and historical trends help your team act before small issues become outages.
Dedicated VLANs and segmentation that keep IoT sensors, PLCs and automation devices isolated from corporate traffic. This protects operational technology while still allowing controlled data flow to your ERP and analytics systems.



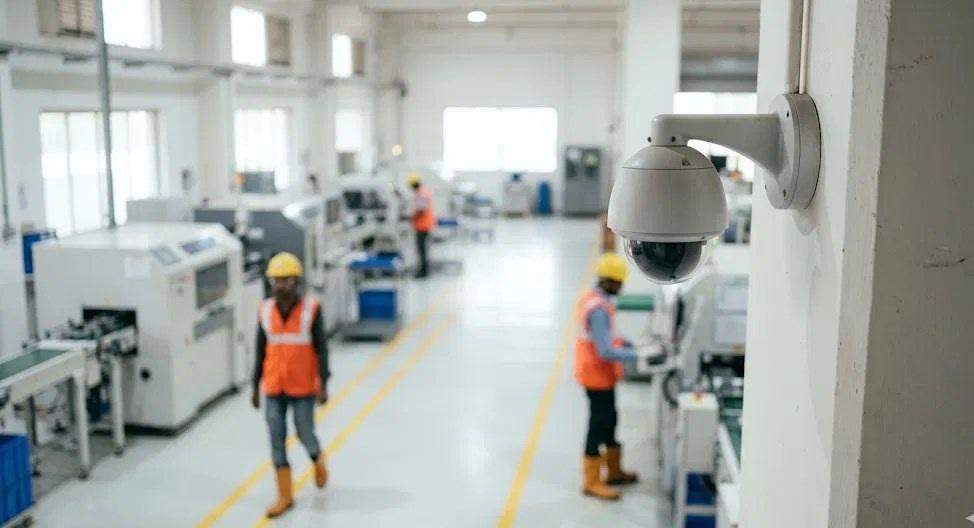
Comprehensive IP camera coverage of production areas, warehouses, entry gates and parking lots — with high-resolution recording, remote viewing and intelligent video analytics built in.
Vandal-resistant, wide-angle fixed cameras for indoor production and assembly halls. High-resolution sensors capture clear detail for incident review, quality disputes and process documentation.
Pan-tilt-zoom units that cover large warehouses, open yards and perimeter fencing from one mounting point. Operators can follow movement live or set automatic patrol patterns across wide areas.
Network video recorders with RAID-protected storage and configurable retention periods to meet audit and compliance requirements. Footage stays safe even if a single drive fails.
Long-range infrared illuminators and low-light sensors deliver usable footage in unlit yards and night shifts. Coverage stays consistent around the clock, not just during daylight hours.
A secure web portal and mobile app for real-time monitoring and playback from any location. Plant heads and security teams can check any camera without being on site.
Motion zones, line-crossing alerts and loitering detection turn passive cameras into an active security tool. The system flags unusual activity at gates, stores and restricted zones instead of relying on constant manual watching.


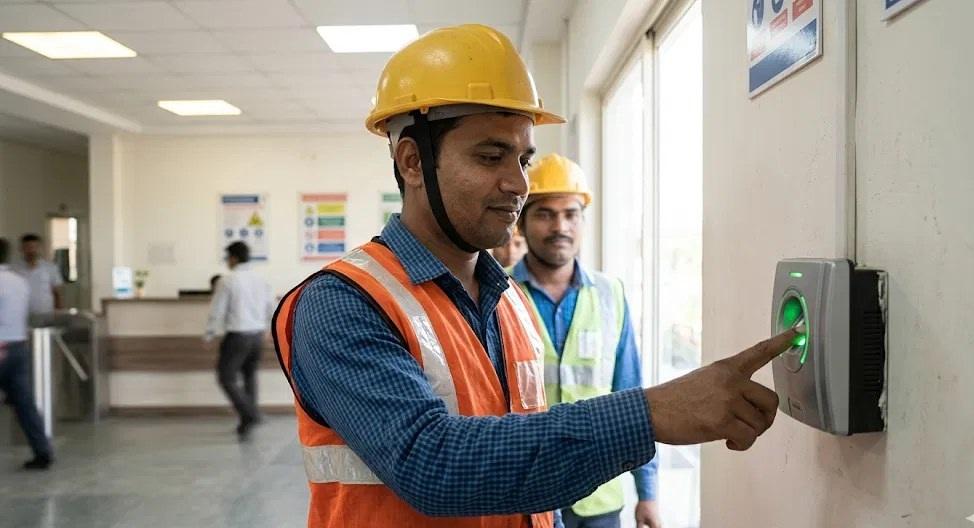
Accurate, tamper-proof attendance capture for permanent staff and contract labour across every shift — with software that feeds directly into payroll and consolidates data across all your sites.
Ruggedised readers built to perform reliably in oily, dusty and humid factory conditions where ordinary scanners fail. Fast one-touch verification keeps shift-change queues moving.
Touchless face-ID terminals ideal for high-throughput entry points and hygiene-sensitive areas. Workers are identified in under a second without contact, gloves removed or cards needed.
A shift-wise dashboard covering attendance, contractor tracking, late marks and overtime in one place. Managers get accurate headcounts per line and per shift without manual registers.
Direct, formatted integration with SAP, Tally and other payroll platforms. Attendance data flows straight into salary processing, removing re-keying errors and month-end delays.
Centralised, real-time consolidation of attendance data across every plant location. Head office sees a single unified view rather than separate spreadsheets from each unit.
Online pre-registration for contractors and visitors with time-limited access credentials. Approvals, ID capture and gate notification happen before the person even arrives.
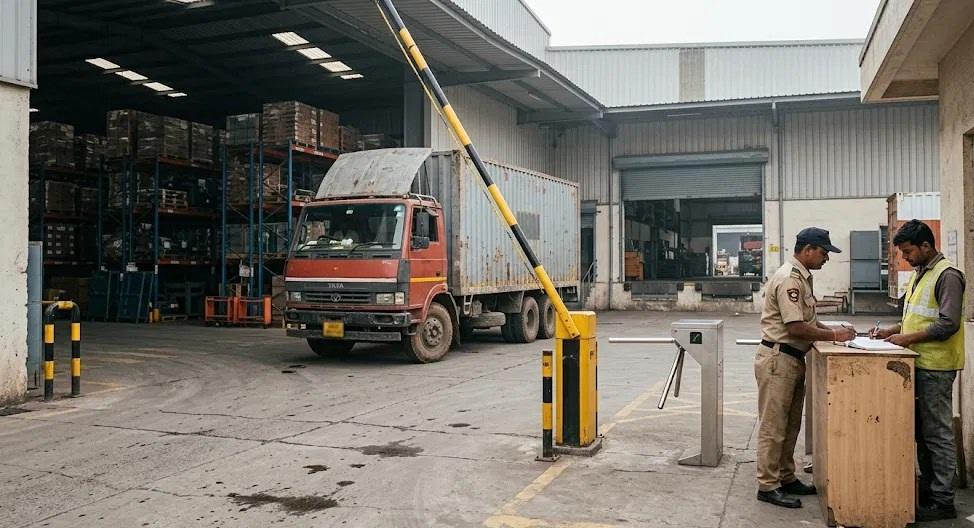
Controlled, auditable entry to every gate, door and restricted zone — covering staff, vehicles, contractors and visitors with a complete exportable record of who went where, and when.
RFID cards and fobs that grant staff access only to the zones their role requires. Lost cards are deactivated instantly, and permissions can be changed centrally without re-issuing hardware.
Fingerprint and face-ID controllers for server rooms, stores and other high-value areas. Access is tied to the individual, so credentials cannot be shared or passed on.
Vehicle boom barriers and pedestrian turnstiles that enforce orderly, controlled flow at main and service gates. Only authorised people and vehicles pass, and tailgating is physically prevented.
A self-service kiosk that scans ID, prints a photo badge and alerts the host by SMS on arrival. Visitor handling becomes faster, more professional and fully logged.
Time-bound credentials for third-party vendors and maintenance crews that expire automatically when the job window ends. No need to chase contractors to return passes.
A complete, searchable entry and exit history for every person, area and time window. Reports export cleanly for safety audits, incident investigations and compliance reviews.
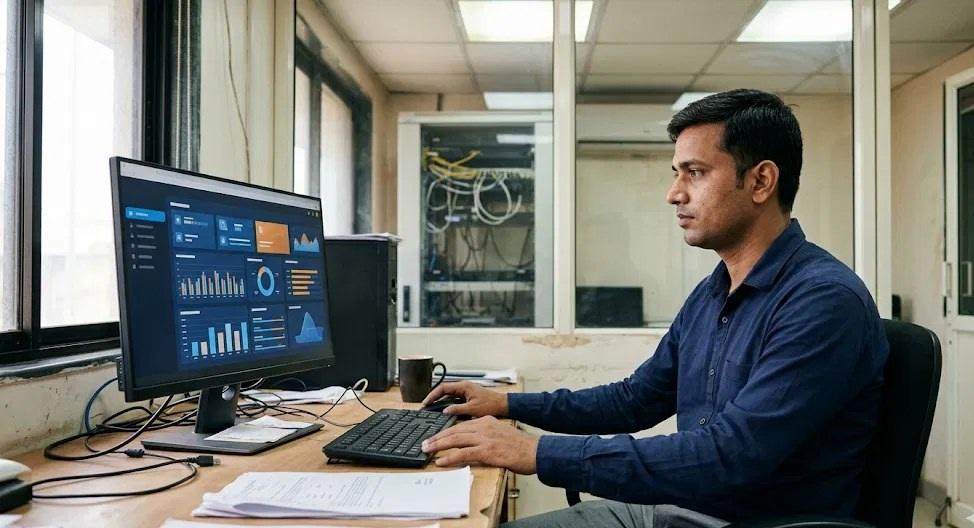
Layered protection for production data, ERP systems and corporate communications — defending against ransomware, insider threats and external intrusion, with OT and IT networks kept properly separated.
An NGFW appliance with intrusion prevention, application awareness and deep-packet inspection at the network edge. It blocks threats by behaviour, not just by port, and reports clearly on what it stops.
A dedicated DMZ and VLAN separation that isolates production machinery and PLCs from the corporate LAN. A malware outbreak on an office PC cannot spread to the line — and vice versa.
Managed antivirus and endpoint detection across every workstation and server, with central visibility of threats. Suspicious activity is identified and contained before it spreads.
DLP policies that restrict sensitive drawings, costings and customer data from leaving via USB drives or personal email. Intellectual property stays inside the company.
Anti-spam and anti-phishing protection for every staff mailbox, filtering malicious links and attachments before delivery. This closes the most common entry point for ransomware.
Periodic network scans with clear patch-status reports and prioritised remediation guidance. You get an honest picture of where the gaps are and a practical plan to close them.


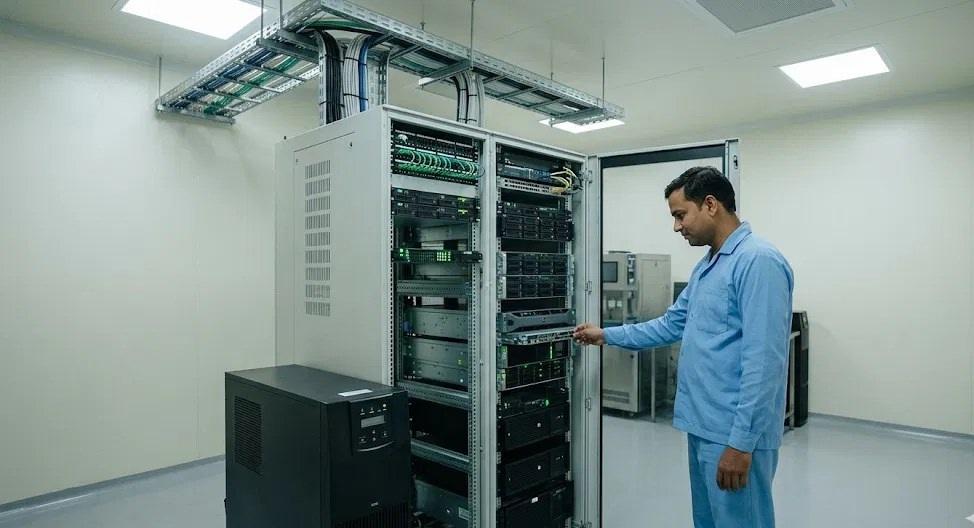
Reliable on-premise compute and storage for ERP, file services and virtualisation — backed by automated, tested backups and a documented disaster-recovery plan that keeps the business running.
HP, Dell and Lenovo servers correctly sized for your ERP, file services and virtualisation workloads. Right-sizing avoids both performance bottlenecks and money wasted on excess capacity.
Centralised storage arrays with RAID protection, tiering and snapshot capability. Critical data is consolidated, protected against drive failure and easy to recover to an earlier point.
Scheduled daily and weekly backups to both on-site and off-site destinations, running without manual intervention. Backups happen reliably even when staff are busy or absent.
Replication paired with a documented DR runbook and restore drills at agreed intervals. Recovery is a tested, rehearsed process — not a hope — when something goes wrong.
Correct Microsoft 365, Windows Server and SQL Server licensing, supplied and deployed. You stay fully compliant and audit-ready, with no licensing surprises.
VMware or Hyper-V virtualisation that consolidates multiple workloads onto fewer physical servers. This cuts hardware cost, power and rack space while making systems easier to back up and restore.




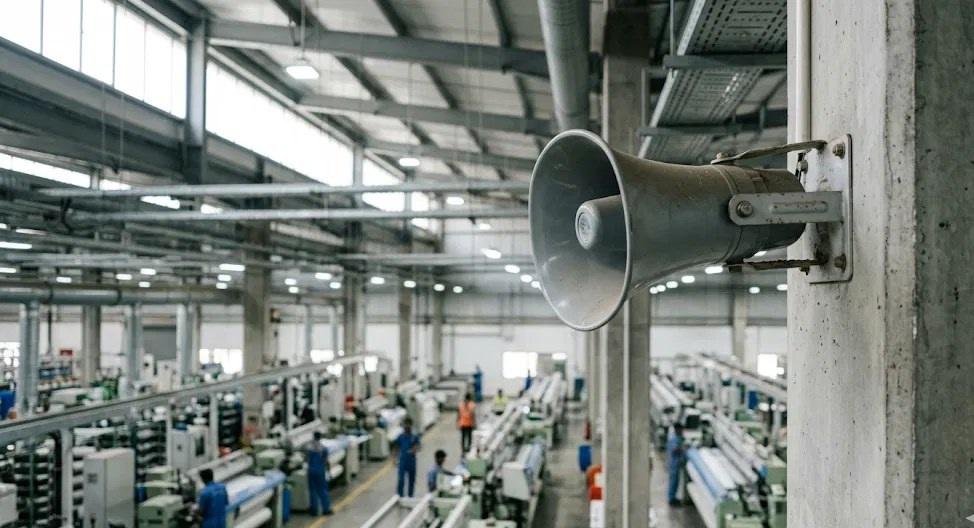
Clear, zoned audio for shift management, routine announcements and emergency evacuation — engineered to be heard over machinery and linked directly to your fire-alarm system.
Independent audio zones for each production block, warehouse and yard, controlled from one matrix amplifier. Broadcasts reach only the zones that need them, without disrupting the whole plant.
Network-based paging with scheduled bulletins and live override from the control room. Messages can be triggered from any authorised station across the site.
Automatic broadcast of evacuation messages across every zone the moment the fire panel triggers. Emergency communication does not depend on someone reaching a microphone.
Weatherproof 100V-line horn speakers rated to cut through high-noise production and outdoor environments. Spoken messages stay intelligible where ordinary speakers would be drowned out.
Programmable shift-change bells and timed chimes that run automatically to a set schedule. Shift discipline is maintained without manual operation.
A staff intercom network linking the security gate, control room and key production stations. Critical two-way communication stays available even if phones or data are down.

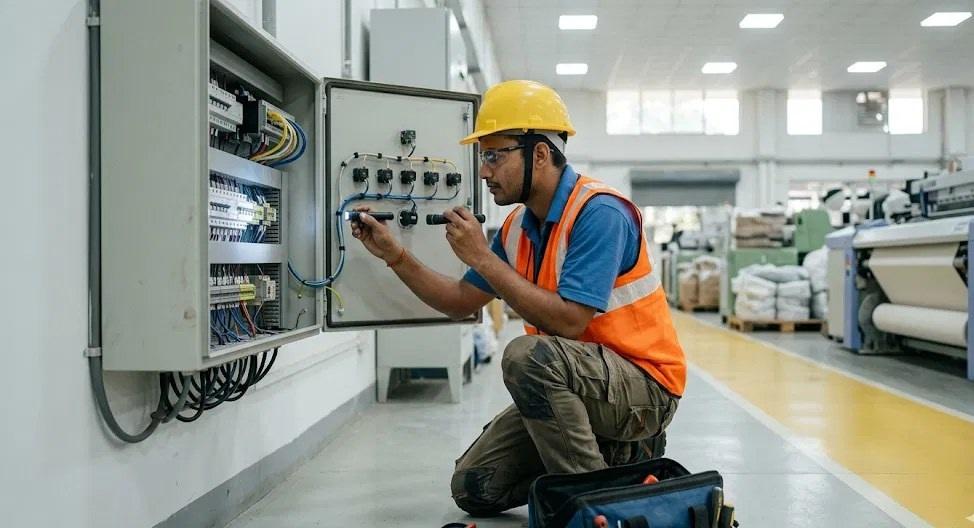
A structured AMC programme that keeps every system performing — combining scheduled preventive visits, remote monitoring and guaranteed response times with a clear escalation path.
Scheduled quarterly or half-yearly on-site inspections and health checks for all covered systems. Wear, faults and ageing components are caught and corrected before they cause a breakdown.
Guaranteed response SLAs for critical faults, so urgent issues are attended within a committed time. Downtime on production-critical systems is kept to a minimum.
Round-the-clock remote visibility of key systems, with issues flagged proactively. Many problems are identified and resolved before your team even notices them.
Critical spares stocked at our depots ready for rapid swap-out. Restoration does not wait on procurement lead times or import delays.
As-built drawings, asset registers and maintenance logs kept current and on hand. Audits, expansions and handovers are straightforward because the records are always accurate.
A defined escalation matrix running from field engineer up to senior management. If an issue is not resolved at one level, it moves up automatically — you are never left without a contact.
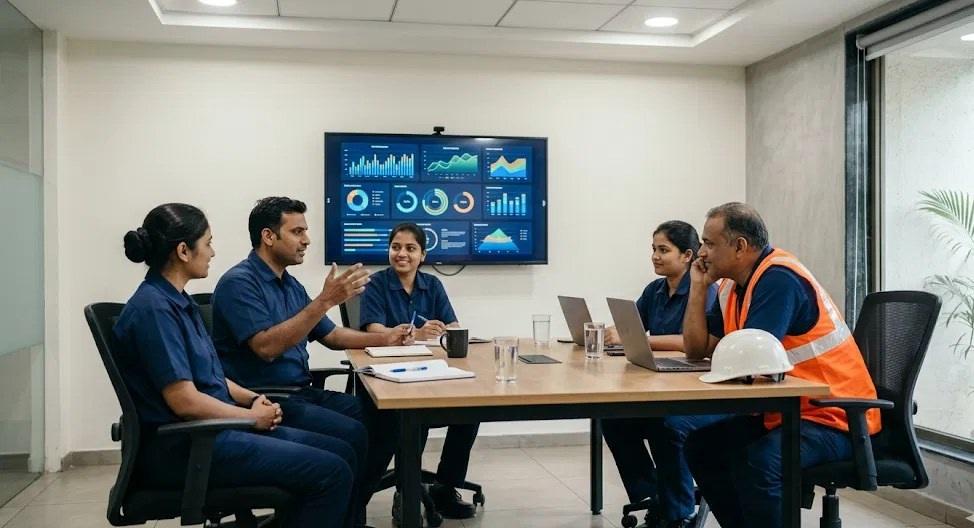
Professional meeting-room AV, wireless presentation and plant-wide digital signage — keeping leadership connected and the shop floor informed with live operational data.
Large-format displays, PTZ cameras, directional microphones and conferencing software set up as one integrated system. Meetings start on time and look professional, on screen and in the room.
Barco ClickShare or equivalent that lets anyone present from a laptop or phone without cables or adapters. Sharing content takes seconds, regardless of the device brought into the room.
Industrial-grade screens showing live OEE, output targets, downtime and quality alerts. Operators and supervisors see real performance data without leaving the line.
Centralised content management that updates every screen across the plant from one console. Safety messages, notices and dashboards stay current everywhere at once.
A projector or large panel, audio system and interactive annotation for inductions and skill training. Sessions run smoothly without scrambling for working equipment.
Microsoft Teams Rooms, Zoom Rooms or Cisco licensing with endpoint setup and testing. Remote meetings with customers, group offices and suppliers just work.

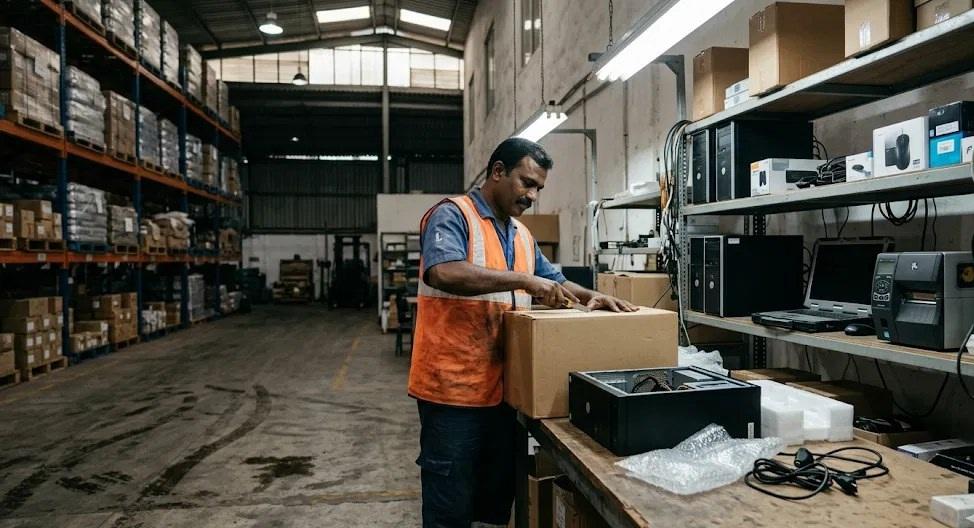
A single trusted source for desktops, laptops, printers, power protection and warehouse peripherals — supplied, tagged, warranty-tracked and responsibly disposed of at end of life.
HP, Dell and Lenovo commercial-grade devices supplied with full OEM warranty. Business-class hardware means fewer failures and a longer, more predictable service life.
Canon, HP and Epson laser and inkjet printers, copiers and multifunction devices for offices and stores. The right device is matched to each location's actual print volume.
Zebra and TSC thermal printers for warehouse, dispatch and inventory labelling. Durable, scannable labels keep stock movement accurate and traceable.
Online UPS units and automatic voltage regulators protecting critical workstations and servers. Equipment is shielded from the surges, sags and outages common on industrial supply.
Barcode or QR tagging of every device, linked to a register with warranty and location tracking. You always know what you own, where it is and when its cover expires.
Certified data-wiping and responsible e-waste disposal of retired equipment. Old hardware leaves the site securely and in line with environmental regulations.
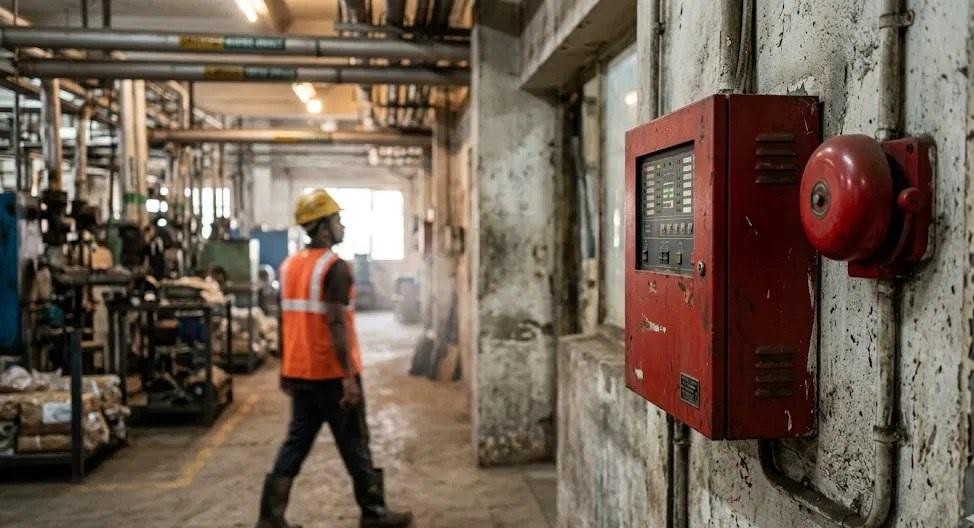
Early, reliable detection of fire and unauthorised entry — built around addressable panels, quality detectors and automatic integration with your evacuation and suppression systems.
Loop-based addressable panels that pinpoint the exact device in alarm or fault. Response teams go straight to the location instead of searching a whole zone.
Optical smoke, rate-of-rise heat and multi-sensor detectors matched to each area's risk profile. Detector type is chosen to suit dust, fumes and temperature so false alarms stay low.
Strategically placed break-glass call points and alarm sounders across the site. Anyone spotting a fire can raise the alarm immediately, and it is heard everywhere.
PIR motion sensors, door contacts and perimeter beam detectors guarding the site after hours. Unauthorised entry is detected and alerted the moment it happens.
Automatic evacuation broadcasts across every PA zone the instant the fire panel triggers. Detection and clear voice instructions act together as one system.
Monitoring interfaces for clean-agent and sprinkler systems in server rooms and other critical areas. The status of suppression systems is visible and supervised at all times.

End-to-end surveillance and access control covering every gate, bay, warehouse and restricted area.
Redundant networking and automated backup keep ERP, production systems and communications running.
Automated biometric attendance eliminates buddy-punching and payroll errors across all shifts.
Single point of accountability for all technology across the plant — from supply to support.
Decades of hands-on experience deploying technology in Indian industry.
Design, supply, installation, integration and ongoing support — one partner.
Deep expertise across manufacturing, education, healthcare, retail and more.
Offices in Mumbai, Goa and Surat; fast on-site response wherever you are.
Take the full catalogue with you, or tell us about your site for a free survey and quote.